Why Is Chemical Manufacturing Important for Global Buyers?

Chemical manufacturing is the upstream engine behind products buyers rely on every day. It turns feedstocks into resins, solvents, fertilizers, coatings, and specialty ingredients. These materials support packaging, construction, electronics, agriculture, and healthcare. A resin pellet or a precise coating additive can affect an entire production line. Small inputs, wide consequences.

The scale is substantial. Cefic’s Facts & Figures 2024 report estimates global chemical sales reached about €5.05 trillion in 2023. That figure signals both the sector’s economic reach and the breadth of its supply networks. But sales value alone does not guarantee reliable supply. Buyers still need to assess product specifications, consistency between batches, delivery capacity, and supplier documentation. One missed shipment can leave expensive equipment idle.

Energy use also deserves attention. The International Energy Agency’s The Future of Petrochemicals identifies petrochemicals as a major driver of future oil demand. This matters to buyers because energy costs, feedstock prices, and production disruptions can influence both lead times and purchasing costs. Supplier location matters, too. A lower quoted price may look attractive until transport delays or limited backup capacity enter the calculation.

For global buyers, understanding chemical manufacturing is therefore a practical sourcing advantage, not just an industry overview. Comparing suppliers requires evidence: current technical data, clear quality controls, and realistic delivery commitments. Even then, forecasts can miss the mark. Resilience is not a guarantee; it is a risk buyers can examine, question, and improve.
Why Is Chemical Manufacturing Important for Global Buyers?

What Chemical Manufacturing Includes

Chemical manufacturing is more than mixing ingredients in a tank. It covers the planned movement of raw materials through controlled processes until they become usable products. A facility may inspect feedstocks, measure them, and use reactions, heating, cooling, or blending to meet a defined specification. Further steps can include separation, filtration, drying, or purification. Not every plant uses every step. Products may then be formulated into a particular concentration, texture, or performance profile. Production also involves equipment maintenance, process monitoring, and controls for worker safety and environmental impact. Quality checks compare samples with agreed specifications. Small changes matter.

For global buyers, manufacturing includes the records and practical checks that help explain how a product was made. Buyers may review test results, batch documentation, packaging details, and storage requirements before arranging shipment. Traceable records can help identify where a batch differs from expectations. Packaging and storage conditions matter too; moisture, temperature, or handling can affect some materials. Manufacturing performance depends on repeatable procedures, but scale-up is not always perfectly smooth. A process can look excellent on paper and still need adjustment when equipment or production volumes change. That gap deserves honest discussion between suppliers and buyers.

How Chemical Products Support Global Industries

Chemical products often work behind the scenes. Fertilizers support crop yields, while polymers and additives help protect food, buildings, cables, and vehicle components. Coatings resist moisture. Insulation reduces heat loss. These materials help manufacturers manage durability, weight, hygiene, and processing speed. That matters when food packaging must seal reliably or a pipe must withstand years of pressure.

Cefic’s Facts & Figures 2024 reports global chemical sales of €5.434 trillion in 2023. China accounted for 43% of that value, while the EU represented 13%. The scale points to a connected supply base, but it does not guarantee local availability. Global buyers therefore assess more than unit price. Purity, concentration, batch consistency, packaging, shelf life, and delivery conditions can all affect production. A small variation in resin viscosity, for example, may change molding time or reject rates. Specifications matter.

The International Energy Agency’s The Future of Petrochemicals identifies chemicals as the largest industrial energy-consuming sector. Energy efficiency can affect both operating costs and environmental performance. Still, product data do not tell the whole story. Transport routes, storage conditions, and supplier documentation also shape reliability; buyers may overlook these until a shipment is delayed. Chemical sourcing is technical, but real supply chains are not always neat.

How Chemical Manufacturing Connects Global Supply Chains

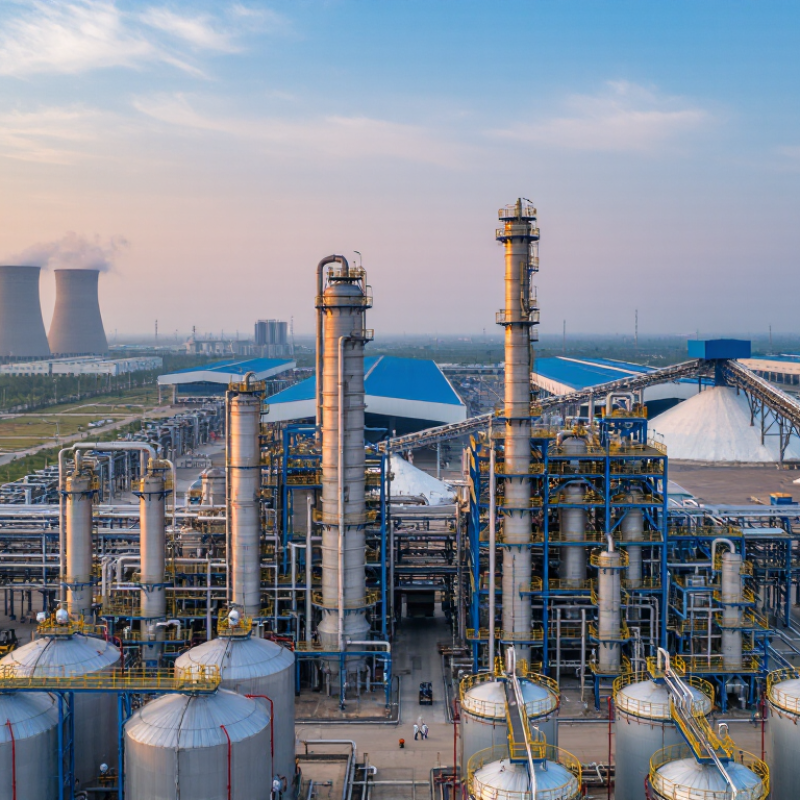
Chemical manufacturing connects mines, refineries, processing plants, ports, and factories. A single material may pass through several countries before reaching a buyer. Cefic’s 2024 Facts & Figures report puts global chemical sales at about €5 trillion in 2023. That scale reflects how many industries depend on chemical inputs, from agriculture and construction to electronics and healthcare.

The links are practical, not abstract. A delayed additive shipment can leave a coating line idle, even when its main ingredients are available. Buyers therefore assess supplier location, transport time, product specifications, and backup inventory together. Small delays travel. The International Energy Agency’s 2018 report, The Future of Petrochemicals, projected that chemicals would account for more than a third of oil-demand growth through 2030. This underlines the sector’s close ties to energy and feedstock supply chains.

Strong coordination also depends on reliable information: clear specifications, consistent quality checks, and realistic delivery schedules. A shipment can arrive on time yet still disrupt production if its grade differs from the approved material. Regional sourcing may reduce transit risk, but it can narrow supplier choice or raise costs. There is no perfect network. Buyers need to understand where key inputs originate and which alternatives have actually been tested.

What Global Buyers Evaluate When Sourcing Chemicals

Why Is Chemical Manufacturing Important for Global Buyers?
What Global Buyers Evaluate When Sourcing Chemicals

Chemical manufacturing supports industries from agriculture and construction to electronics and healthcare. Global buyers need more than a competitive price: they evaluate product consistency, production capacity, delivery reliability, and clear technical documentation. The European Chemical Industry Council reported global chemical sales of about €5 trillion in 2023. That scale reflects a complex market, where small differences in purity or particle size can affect an entire production run.

Quality evidence matters. Buyers often check certificates of analysis, safety data sheets, batch traceability, and whether specifications match their process. They also assess packaging, storage requirements, and contingency plans for delays. The International Energy Agency estimates that chemicals account for around 10% of global final energy demand and 7% of greenhouse gas emissions. These figures make energy use and environmental data relevant sourcing questions, though supplier claims still need careful verification. A cheap quote can cost more later. Documentation is not a formality.

Tips: Request a recent sample and compare it against your own acceptance criteria. Confirm lead times in writing. Check that every document refers to the same grade and batch. If one detail feels unclear, pause and ask; buyers sometimes overlook that step.

Why Is Chemical Manufacturing Important for Global Buyers? — What Global Buyers Evaluate When Sourcing Chemicals
Evaluation Dimension Why It Matters What Buyers Evaluate Useful Evidence or Indicators
Product quality and consistency Consistent chemical properties help buyers maintain reliable processes, product performance, and finished-goods quality. Specification compliance, batch-to-batch variation, impurity limits, and the supplier’s change-control process. Current technical data sheet, certificate of analysis for each batch, agreed acceptance criteria, and documented change notifications.
Manufacturing capability and capacity Production capability affects whether orders can be supplied at the required volume and schedule, including during demand changes. Available production capacity, process controls, equipment suitability, maintenance practices, and ability to scale or accommodate forecasts. Capacity statements, production and quality procedures, lead-time commitments, and a clear process for handling demand fluctuations.
Regulatory compliance Chemicals may be subject to different registration, classification, labeling, and import requirements in destination markets. Compliance with applicable rules for the product, intended use, transport route, and importing country. Safety data sheet, hazard classification and label information, relevant registrations or declarations, and confirmation of current regulatory status.
Health, safety, and environmental management Safe production, handling, and transport reduce risks to workers, communities, and the environment. Hazard controls, worker training, emergency procedures, waste management, emissions controls, and safe handling guidance. Safety data sheet, site safety procedures, environmental permits where applicable, incident-response plans, and audit findings.
Supply reliability and lead time Unpredictable supply can interrupt manufacturing and increase inventory or expediting costs. Production lead time, order-confirmation practices, continuity planning, raw-material dependencies, and communication during disruptions. Documented lead times, delivery-performance records, business-continuity plans, and agreed escalation contacts.
Logistics and transport suitability Chemical shipments must use packaging and transport arrangements suited to the product’s hazards and delivery conditions. Packaging compatibility, labeling, shipment mode, temperature or moisture requirements, and dangerous-goods documentation where applicable. Packaging specifications, transport classification, shipping documents, and instructions for storage and handling in transit.
Traceability and documentation Traceable records support quality investigations, regulatory inquiries, recalls, and verification of product origin and batch history. Batch identification, retention of production records, document accuracy, and the ability to link shipments to test results. Batch numbers, certificates of analysis, production-date records, shipment records, and a documented complaint or recall process.
Total landed cost The purchase price is only one part of cost; freight, duties, insurance, packaging, storage, and quality-related losses can also affect the total. Quoted price basis, currency and payment terms, freight responsibility, taxes or duties, packaging costs, and potential cost of nonconformance. Itemized quotations, agreed trade terms, freight estimates, import-cost calculations, and clearly defined quality remedies.
Technical support and communication Responsive technical communication helps buyers confirm product suitability, resolve process issues, and manage specification changes. Access to qualified technical contacts, response times, language and time-zone coverage, and support during trials or troubleshooting. Defined communication channels, technical documentation, sample or trial procedures, and documented response and escalation arrangements.
Supplier risk and business continuity Assessing operational, geographic, and financial dependencies helps buyers prepare for disruptions and protect continuity of supply. Production-site concentration, critical input dependencies, contingency arrangements, financial and operational stability, and visibility into subcontracting. Risk assessments, contingency plans, disclosure of relevant production locations, and periodic supplier-performance reviews.

How Manufacturing Changes Affect Global Buyers

Changes on a chemical production line can affect buyers before a shipment leaves the plant. A reactor upgrade, maintenance shutdown, or new process control may alter output, lead times, or batch availability.

Small shifts matter.

A coatings producer waiting for a resin drum may need to reschedule mixing and packaging when delivery slips by a week. Buyers should ask whether quoted dates reflect current capacity, planned maintenance, and feedstock supply, not just past performance.

Process changes can also affect specifications. Different equipment settings or raw-material sources may influence color, viscosity, moisture, or purity, even when a product name stays the same. Request updated specifications, change notices, and relevant test data before approving a substitute.

Keep a retained sample where practical. It helps resolve disputes later. Still, paperwork alone is not proof; incoming checks and clear acceptance limits matter.

A newer process is not automatically more reliable, and extra inventory ties up cash. Forecasts can be wrong, too. That is uncomfortable, but realistic. Buyers who compare supplier updates with actual delivery records can adjust safety stock and production plans earlier, while keeping a backup option qualified rather than merely listed.